Operating Procedures
- Clean the seat area carefully.
- Coat the seat with machinist’s dye.
- Fit a 45В° cutter into the holder and slide it into the valve guide.
- Press down lightly on the handle and turn it right or left.
NOTICE
Do not grind the seat too much. Overgrinding will reduce valve clearance by sinking the valve into the head. If the valve sinks too far into the head, it will be impossible to adjust the clearance, and the cylinder head must be replaced.
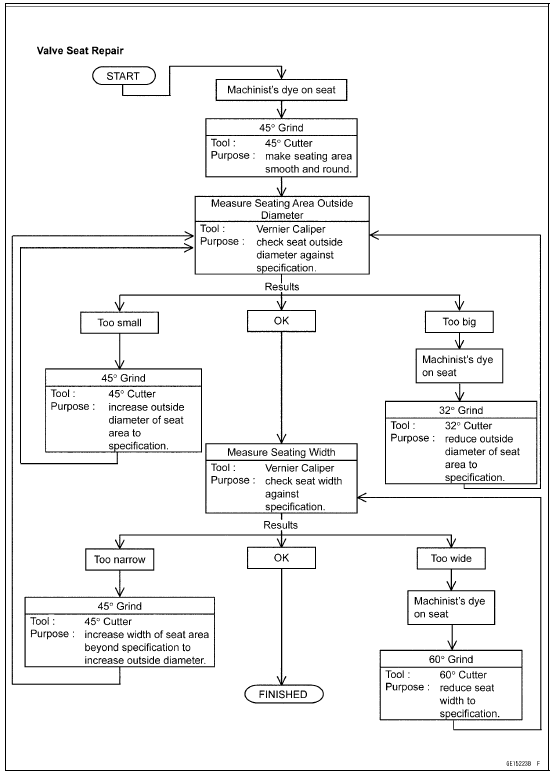
- Measure the outside diameter of the seating surface with a vernier caliper.
If the outside diameter of the seating surface is too small, repeat the 45В° grind until the diameter is within the specified range.
Widened Width [A] of engagement by machining with 45В° cutter
Ground Volume [B] by 32В° cutter 32В° [C]
Correct Width [D]
Ground Volume [E] by 60В° cutter 60В° [F]
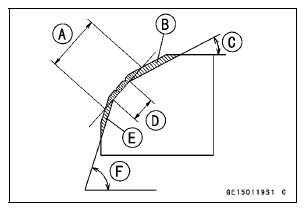
- Measure the outside diameter of the seating surface with a vernier caliper.
If the outside diameter of the seating surface is too small, repeat the 45В° grind [A] until the diameter is within the specified range.
Original Seating Surface [B]
NOTE
- Remove all pittings of flaws from 45В° ground surface.
- After grinding with 45° cutter, apply thin coat of machinist’s dye to seating surface. This makes seating surface distinct and 32° and 60° grinding operation easier.
- When the valve guide is replaced, be sure to grind with 45В° cutter for centering and good contact.
If the outside diameter [A] of the seating surface is too large, make the 32В° grind described below.
If the outside diameter of the seating surface is within the specified range, measure the seat width as described below.
- Grind the seat at a 32В° angle [B] until the seat outside diameter is within the specified range.
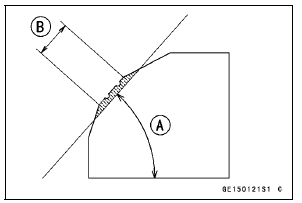
To make the 32В° grind, fit a 32В° cutter into the holder, and slide it into the valve guide.
Turn the holder one turn at a time while pressing down very lightly. Check the seat after each turn.
NOTICE
The 32В° cutter removes material very quickly.
Check the seat outside diameter frequently to prevent overgrinding.
After making the 32В° grind, return to the seat outside diameter measurement step above.
- To measure the seat width, use a vernier caliper to measure the width of the 45В° angle portion of the seat at several places around the seat.
If the seat width is too narrow, repeat the 45В° grind until the seat is slightly too wide, and then return to the seat outside diameter measurement step above.
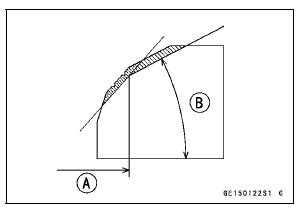
If the seat width is too wide, make the 60В° [A] grind described below.
If the seat width is within the specified range, lap the valve to the seat as described below.
- Grind the seat at a 60В° angle until the seat width is within the specified range.
To make the 60В° grind, fit 60В° cutter into the holder, and slide it into the valve guide.
Turn the holder, while pressing down lightly.
After making the 60В° grind, return to the seat width measurement step above.
Correct Width [B]

NOTICE
Do not lap the valve to the valve seat, using the grinding compound. It will come off oxide film treated surface of the valve.
- When the engine is assembled, be sure to adjust the valve clearance (see Valve Clearance Inspection in the Periodic Maintenance chapter).
Test yourself
A quick Kawasaki Ninja ZX-10R quiz: every answer comes with an explanation and a link to the manual page.