Machining Valve Seats in Cylinder Head / Valve Lapping
Valve seat machining is required if the seats show signs of wear or burning, or if the guides have been machined. The correction angle and seat width must be observed. Replacing the seats with conventional tools is not possible, since they are installed after cooling to -150°C. A special machine is required to machine the seat. This work must be performed at a workshop. Machining angles are given in the Specifications.
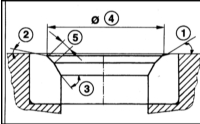
* The outer diameter of the valve seat (4) corresponds to the outer diameter of the valve.
Valve Seat Lapping
If the valve seats are machined correctly and new valves are used, lapping of the seats in the cylinder head is not required.
Valves must be lapped only with fine-grit lapping compound. For lapping, use a suction cup attached to the valve head. During lapping, frequently lift the valve while rotating it. This prevents grooves from forming on the lapped surface.
* After lapping, carefully remove all compound from the valve.
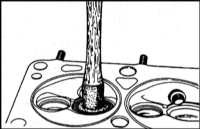
The lapping quality can be checked visually and with fuel. To do this, insert the valve loosely into the inverted cylinder head and pour fuel into the combustion chamber from above. After a long period (1 hour), fuel must not leak past the valve seat. Otherwise, repeat the lapping.
Test yourself
A quick BMW 1 quiz: every answer comes with an explanation and a link to the manual page.