Filler
2K HS Variofiller
Designation:
- 2K HS Variofiller -LGF 786 004 A4-, colour grey
Product description
The 2K HS Variofiller is a high-quality, variable, VOC-compliant 2K HS filler based on acrylic resin.
Features:
- can be used as a sanding filler and as a wet-on-wet filler
- can be used with HS and VHS hardeners
- good insulating properties, including over thermoplastic old paint
- very good paint stability
Application information
Substrate
Suitable substrates:
- cleaned and sanded steel panels primed with 2K wash primer -LHV 043 000 A2- or 1K wash primer -LVM 044 007/171 A2-, electrolytically/galvanically galvanized steel panels, or soft aluminium
- lightly or unsanded, thoroughly cleaned original factory primer
- cleaned and sanded, electrogalvanized steel panels or soft aluminum
- sanded factory or old paint (including thermoplastic coatings)
- surfaces pre-worked with 2K polyester products and then finely sanded
- cleaned and sanded UP-GF substrates free of release agents
Pretreatment of substrates:
- Clean thoroughly with silicone remover -LVM 020 000 A5- or long-acting silicone remover -LVM 020 100 A5-.

- Then sand.
- Use a suitable cleaner before overcoating to ensure a clean, residue-free surface.
Application with intermediate sanding
Mixing ratio:
- 5:1 by volume with:
- 2K VHS hardener -LHA 009 051 A2-/-LVM 009 051 A5-
- 2K VHS hardener, long -LHA 009 052 A2-/-LHA 009 052 A3-
- 2K VHS hardener, extra long -LHA 009 053 A2-
Mixing ratio:
- 3:1 by volume with:
- 2K HS hardener, short -LHA 021 004 A3-
- 2K HS hardener -LHA 009 041 A3-
- 2K HS hardener, long -LHA 009 047 A3-
- 2K HS hardener, extra long -LHA 009 048 A3-
Elasticizing, see

Processing/pot life:
- Ready-to-spray mixture 30-60 minutes at +20 °C (depending on the hardener used)
Thinner:
- 2K thinner -LVE 009 001 A5-
- 2K thinner, long -LVM 009 300 A2-
- 2K thinner, plus -LHA 014 000 A5-
- 2K thinner, special -LVM 009 200 A2/A5-
Application method "Spray pass"

- Application viscosity 4 mm at +20 °C, DIN 53211
Application viscosity, 4 mm flow cup, "Compliant" and "HVLP" spray guns:
DIN 4 mm: 20-25 seconds
Hardener addition at +20 °C material temperature of 10-15 % HS hardener or 10-20 % VHS hardener
- When adding hardener, use a measuring stick for mixing.
- Set the spray nozzle (see manufacturer's specifications): "Compliant" 1.4-1.8 mm.
- Set the spray nozzle (see manufacturer's specifications): "HVLP" 1.6-1.9 mm.
- Set the spray pressure (see manufacturer's specifications): "Compliant" 1.5-3.0 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- 2 spray passes are required to achieve a dry film thickness of 50-80 µm.
- 3 spray passes are required to achieve a dry film thickness of 100-120 µm.
- The recommended dry film thickness is 50-120 µm.
Drying with intermediate sanding
Air drying at +20 °C room temperature, can only be sanded after overnight drying
The final flash-off time with forced drying is at least 5-10 minutes.
Forced drying at +60 °C object temperature: up to 80 µm for 20-30 minutes and above 80 µm for 40-45 minutes

The final flash-off time with infrared drying is at least 5-10 minutes.
Infrared drying (depending on film thickness): medium-wave emitter 10-20 minutes and short-wave emitter 10 minutes
Further processing
- Dry sanding with dual-action sander and dust extraction, abrasive paper grit P400-500
- Wet sanding with abrasive paper grit P800-1000

Rework with intermediate sanding
Can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat

Application as a "wet-on-wet" filler
Mixing ratio:
- 5:1 by volume with:
- 2K VHS hardener -LHA 009 051 A2-/-LVM 009 051 A5-
- 2K VHS hardener, long -LHA 009 052 A2-/-LHA 009 052 A3-
- 2K VHS hardener, extra long -LHA 009 053 A2-
Mixing ratio:
- 3:1 by volume with:
- 2K HS hardener, short -LHA 021 004 A3-
- 2K HS hardener -LHA 009 041 A3-
- 2K HS hardener, long -LHA 009 047 A3-
- 2K HS hardener, extra long -LHA 009 048 A3-
Processing/pot life:
- Ready-to-spray mixture 30-60 minutes at +20 °C (depending on the hardener used)
Thinner:
- 2K thinner -LVE 009 001 A5-
- 2K thinner, long -LVM 009 300 A2-
- 2K thinner, plus -LHA 014 000 A5-
- 2K thinner, special -LVM 009 200 A2/A5-

Application method "Spray pass"
- Application viscosity 4 mm at +20 °C, DIN 53211
Application viscosity, 4 mm flow cup, "Compliant" and "HVLP" spray guns:
DIN 4 mm: 16-18 seconds
Hardener addition at +20 °C material temperature of 20-25 % HS hardener or 30 % VHS hardener
- When adding hardener, use a measuring stick for mixing.
- Set spray nozzle (see manufacturer's data): "Compliant" 1.2-1.4 mm.
- Set spray nozzle (see manufacturer's data): "HVLP" 1.3-1.5 mm.
- Set spray pressure (see manufacturer's specifications): "Compliant" 2.0–2.5 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- The recommended dry film thickness is 25-30 µm. 1-2 spray passes are required to achieve this.
"Wet-on-wet" application
Flash-off time before topcoat application at +20 °C room temperature:
15-20 minutes up to a maximum of 90 minutes with 2K HS topcoat
25-30 minutes up to a maximum of 90 minutes with waterborne basecoat
30-35 minutes up to a maximum of 90 minutes with Aqua Premium waterborne basecoat
Rework as a "wet-on-wet" filler
Can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat
Special Notes
Elasticizing of rigid and semi-rigid plastics:
- The base material must first be mixed with 15 % elasticizer -ALZ 011 001-. 3:1 mixing ratio with VHS hardeners and 20 % thinner; 2:1 mixing ratio with HS hardeners and 20 % thinner.
- Any defects in the substrate can be spot-filled with 2K polyester filler. After drying and intermediate sanding, seal the filled areas with 2K HS Variofiller.
- To achieve an optimal surface finish on passenger car paintwork, we recommend sanding the filler after air drying overnight.
- Do not use wet-on-wet application on thermoplastic factory paint, and sand the filler after air drying overnight if possible.
- For air drying, a minimum temperature of +15 °C is recommended.

Caution!
Flash-off times before applying basecoat/2K topcoat series increase to 30-40 minutes.
Personal protective equipment:
- Observe the safety data sheet
- Wear personal protective equipment during application
Characteristics


Storage
Guaranteed storage stability is 24 months from production date. Use by the date stated on the label at the latest when stored in sealed original containers at +20 °C.
2K HS Premium Filler
Designation:
- 2K HS Premium Filler -LVM 013 171 A4-, color dark gray
- 2K HS Premium Filler -LGF 013 007 A4-, color light gray
- 2K HS Premium Filler -LGF 013 100 A4-, color white
- 2K HS Premium Filler -LGF 013 190 A4-, color anthracite
Product description
These 2K HS Premium fillers are very high-quality 2K HS sanding fillers based on acrylic resin.
Features:
- very long pot life
- optimal and safe processing properties
- excellent sandability
- excellent sag resistance
- very high coverage
- excellent filling power
- excellent paint stability
Application information
Substrate
Suitable substrates:
- cleaned and sanded steel panels primed with 2K wash primer -LHV 043 000 A2- or 1K wash primer -LVM 044 007/171 A2-, electrolytically/galvanically galvanized steel panels, or soft aluminium
- lightly or unsanded, thoroughly cleaned original factory primer
- sanded factory or old paint (including thermoplastic coatings)
- surfaces pre-worked with 2K polyester products and then finely sanded
- cleaned and sanded UP-GF substrates free of release agents
Pretreatment of substrates:
- Clean thoroughly with silicone remover -LVM 020 000 A5- or long-acting silicone remover -LVM 020 100 A5-.
- Then sand.

- Use a suitable cleaner before overcoating to ensure a clean, residue-free surface.
Processing
Mixing ratio:
- 4:1 by volume with:
- 2K HS hardener -LHA 009 041 A3-
- 2K HS hardener, short -LHA 021 004 A3-
- 2K HS Hardener, extra short -LHA 009 046 A2-
- 2K HS hardener, long -LHA 009 047 A3-
- 2K HS hardener, extra long -LHA 009 048 A3-
Mixing ratio:
- 7:1 by volume with:
- 2K VHS Hardener, short -LHA 009 050 A2-
- 2K VHS hardener -LHA 009 051 A2-/-LVM 009 051 A5-
- 2K VHS hardener, long -LHA 009 052 A2-/-LHA 009 052 A3-
- 2K VHS hardener, extra long -LHA 009 053 A2-
Elasticizing, see
Processing/pot life:
- Spray-ready setting: 90-120 minutes at +20 °C (depending on the hardener used).
Thinner:
- 2K thinner -LVE 009 001 A5-
- 2K thinner, long -LVM 009 300 A2-
- 2K thinner, plus -LHA 014 000 A5-
- 2K thinner, special -LVM 009 200 A2/A5-
Application method "Spray pass"
- Application viscosity 4 mm at +20 °C, DIN 53211
Processing viscosity, 4 mm flow cup "Compliant" and "HVLP": mixing viscosity.
Hardener addition at +20 °C material temperature: 10 % VHS hardener.
Addition of HS hardener is not required, but up to 10 % is possible.
- When adding hardener, use a measuring stick for mixing.

- Set spray nozzle (see manufacturer's specifications): "Compliant" 1.6-1.8 mm.
- Set spray nozzle (see manufacturer's specifications): "HVLP" 1.5-1.9 mm.
- Set the spray pressure (see manufacturer's specifications): "Compliant" 1.5-3.0 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- To achieve a dry film build of 80-300 μm, 3 spray passes are required.
The maximum dry film build with air drying is 300 μm.
The maximum dry film build with forced drying is 250 μm.
The maximum dry film build with IR drying (color white and light gray) is 200 μm.
The maximum dry film build with IR drying (color black) is 180 μm.
The recommended dry film build is 80-200 μm.
Drying
The material can be sanded after 3-4 hours (film build 80-150 μm, after air drying at +20 °C room temperature).
If film builds of 150-300 μm have been applied, dry overnight before sanding.
The final flash-off time with forced drying is at least 5-15 minutes.
Forced drying at +60 °C object temperature: 80-150 μm 25-30 minutes and 150-250 μm 35-40 minutes.

The final flash-off time with infrared drying is at least 5-15 minutes.
Infrared drying (depending on film build): medium-wave emitter 15-20 minutes and short-wave emitter 10-15 minutes.
Further processing
- Dry sanding with dual-action sander and dust extraction, abrasive paper grit P400-500
- Wet sanding with abrasive paper grit P800-1000
Overcoating
Can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat
Special Notes
Elasticizing of rigid and semi-rigid plastics:
- The base material must first be mixed with 15 % elastic additive -ALZ 011 001-. 3:1 mixing ratio with HS hardeners without thinning, 4:1 mixing ratio with VHS hardeners and 5 % thinning.
- Any defects in the substrate can be spot-filled with 2K polyester putty. After drying and intermediate sanding, isolate the putty areas with 2K HS Premium Filler.
- The best isolation effect (including on critical substrates) is achieved with a medium film build of 80-120 μm in 2 spray passes, with air drying overnight or oven or infrared drying. On critical substrates, fine preparation is required and the parts must be filled over the entire surface.
- For isolating thermoplastic paint systems, we recommend the 2K HS Variofiller -LGF 786 004 A4-, color gray.

Personal protective equipment:
- Observe the safety data sheet
- Wear personal protective equipment during application
Characteristics

Storage
Guaranteed storage stability is 24 months from production date. Use by the date stated on the label at the latest when stored in sealed original containers at +20 °C.
2K HS Mix Filler
Designation:
- 2K HS Mix Filler -LGF 810 150 A4-, color white
- 2K HS Mix Filler -LGF 810 151 A4-, color black
- 2K HS Mix Filler -LGF 810 152 A4-, color red
- 2K HS Mix Filler -LGF 810 153 A2-, color yellow
- 2K HS Mix Filler -LGF 810 154 A2-, color blue
- 2K HS Mix Filler -LGF 810 155 A2-, color green
Product description
The 2K HS Mix Filler system is an innovative, colored 2K HS filler system based on acrylic resin of the latest generation.
The system consists of 6 colored fillers (white, black, yellow, red, green, blue). These can be mixed with each other using simple formulas.
In all settings, this product complies with VOC regulations.
Features:
- suitable for use as interior color and wet-on-wet filler
- excellent, simple and variable processing options
- good flow
- very fast flash-off behavior
- very good paint stability
- excellent sag resistance
- very high coverage
- suitable for use as sanding filler
- good sandability
- excellent filling power
- very good drying properties
- long pot life
Application information
Substrate
Suitable substrates:
- cleaned and sanded steel panels primed with 2K wash primer -LHV 043 000 A2- or 1K wash primer -LVM 044 007/171 A2-, electrolytically/galvanically galvanized steel panels, or soft aluminium
- lightly or unsanded, thoroughly cleaned original factory primer
- sanded factory or old paint finish (except TPA)
- surfaces pre-worked with 2K polyester products and then finely sanded
- cleaned and sanded UP-GF substrates free of release agents
Pretreatment of substrates:
- Clean thoroughly with silicone remover -LVM 020 000 A5- or long-acting silicone remover -LVM 020 100 A5-.

- Then sand.

- Use a suitable cleaner before overcoating to ensure a clean, residue-free surface.

Processing as interior color
Mixing ratio:
- 2:1 by volume with:
- 2K HS hardener -LHA 009 041 A3-
- 2K HS hardener, short -LHA 021 004 A3-
- 2K HS Hardener, extra short -LHA 009 046 A2-
- 2K HS hardener, long -LHA 009 047 A3-
- 2K HS hardener, extra long -LHA 009 048 A3-
- 2K HS Hardener, special -LHA 009 049 A3-
Mixing ratio:
- 3:1 by volume with:
- 2K VHS Hardener, short -LHA 009 050 A2-
- 2K VHS hardener -LHA 009 051 A2-/-LVM 009 051 A5-
- 2K VHS hardener, long -LHA 009 052 A2-/-LHA 009 052 A3-
- 2K VHS hardener, extra long -LHA 009 053 A2-
Processing/pot life:
- Spray-ready setting: 50-60 minutes at +20 °C (depending on the hardener used)
Additive:
- Mix Filler Additive -LZS 811 000 A2-
Application method "Spray pass"
- Application viscosity 4 mm at +20 °C, DIN 53211
Processing viscosity, 4 mm flow cup "Compliant" and "HVLP": 16-19 seconds
Additive addition at +20 °C material temperature: 20 % HS hardener and 40 % VHS hardener.
- When adding hardener, use a measuring stick for mixing.
- Set spray nozzle (see manufacturer's data): "Compliant" 1.2-1.4 mm.
- Set spray nozzle (see manufacturer's data): "HVLP" 1.3-1.5 mm.
- Set the spray pressure (see manufacturer's specifications): "Compliant" 1.5-3.0 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- To achieve a dry film build of 30-70 μm, 3 spray passes are required.
Depending on the color shade, more spray passes may be required.

Note
When used as interior color, topcoating with topcoats is not required.
Application as a "wet-on-wet" filler
Mixing ratio:
- 2:1 by volume with:
- 2K HS hardener -LHA 009 041 A3-
- 2K HS hardener, short -LHA 021 004 A3-
- 2K HS hardener, long -LHA 009 047 A3-
- 2K HS hardener, extra long -LHA 009 048 A3-
Mixing ratio:
- 3:1 by volume with:
- 2K VHS hardener -LHA 009 051 A2-/-LVM 009 051 A5-
- 2K VHS hardener, long -LHA 009 052 A2-/-LHA 009 052 A3-
- 2K VHS hardener, extra long -LHA 009 053 A2-
Elasticizing, see
Processing/pot life:
- Spray-ready setting: 60 minutes at +20 °C (depending on the hardener used)
Additive:
- Mix Filler Additive -LZS 811 000 A2-
Application method "Spray pass"

- Application viscosity 4 mm at +20 °C, DIN 53211
Processing viscosity, 4 mm flow cup "Compliant" and "HVLP": 16-19 seconds
Additive addition at +20 °C material temperature: 20-30 % HS hardener and 40-50 % VHS hardener.
- When adding hardener, use a measuring stick for mixing.
- Set spray nozzle (see manufacturer's data): "Compliant" 1.2-1.4 mm.
- Set spray nozzle (see manufacturer's data): "HVLP" 1.3-1.5 mm.
- Set spray pressure (see manufacturer's specifications): "Compliant" 2.0–2.5 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.

- To achieve a dry film build of 30 μm, 1-2 spray passes are required.
Flash-off time for wet-on-wet application before topcoat application at +20 °C room temperature:
- with water-based basecoat 30-120 minutes
- with 2K HS topcoat 15-120 minutes
Fast spot repair system
Flash-off time for wet-on-wet application before topcoat application at +20 °C room temperature:
- with 2K HS Hardener, extra short -LHA 009 046 A2- 15 minutes
- with 2K VHS Hardener, short -LHA 009 050 A2- 15 minutes
Mix Filler Additive -LZS 811 000 A2- addition at +20 °C material temperature: 20-30 % HS hardener and 40-50 % VHS hardener.
- When adding additive, use a dipstick to mix.
Thinner addition at +20 °C material temperature of 10 % 2K thinner, plus -LHA 014 000 A5-
- When adding thinner, use a measuring stick during mixing.
Overcoating
Can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat
Processing as sanding filler
Mixing ratio:
- 4:1 by volume with:
- 2K HS hardener -LHA 009 041 A3-
- 2K HS hardener, short -LHA 021 004 A3-
- 2K HS Hardener, extra short -LHA 009 046 A2-
- 2K HS hardener, long -LHA 009 047 A3-
- 2K HS hardener, extra long -LHA 009 048 A3-
Mixing ratio:
- 7:1 by volume with:
- 2K VHS Hardener, short -LHA 009 050 A2-
- 2K VHS hardener -LHA 009 051 A2-/-LVM 009 051 A5-
- 2K VHS hardener, long -LHA 009 052 A2-/-LHA 009 052 A3-
- 2K VHS hardener, extra long -LHA 009 053 A2-
Elasticizing, see
Processing/pot life:
- Sprayable after 90-120 minutes at +20 °C (depending on the hardener used)
Thinner:
- 2K thinner -LVE 009 001 A5-
- 2K thinner, long -LVM 009 300 A2-
- 2K thinner, plus -LHA 014 000 A5-
- 2K thinner, special -LVM 009 200 A2/A5-
Application method "Spray pass"
- Application viscosity 4 mm at +20 °C, DIN 53211
Processing viscosity: 4 mm flow cup, "Compliant" and "HVLP" gun, 18-20 seconds
Hardener addition at +20 °C material temperature of 15 % HS hardener and 25 % VHS hardener
- When adding hardener, use a measuring stick for mixing.
- Set the spray nozzle (see manufacturer's specifications): "Compliant" 1.3-1.7 mm.
- Set spray nozzle (see manufacturer's data): "HVLP" 1.3-1.5 mm.
- Set spray pressure (see manufacturer's specifications): "Compliant" 2.0–2.5 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- To achieve a maximum dry film thickness of 200 µm, 2-4 spray passes are required (depending on the spray nozzle).
The maximum dry film thickness with air drying is 200 µm.
The maximum dry film thickness with forced drying is 150 µm.
The maximum dry film thickness with infrared drying (light colours) is 150 µm.
The maximum dry film thickness with infrared drying (dark colours) is 120 µm.
Drying
The material can be sanded after 3-4 hours (film thickness of 60-150 µm and after air drying at +20 °C room temperature).
If film thicknesses of 150-200 µm have been applied, allow to dry overnight before sanding.
The final flash-off time with forced drying is at least 5-15 minutes.

Forced drying at +60 °C object temperature, 60-150 µm: 30-35 minutes
The final flash-off time with infrared drying is at least 5-10 minutes.

Infrared drying (depending on film thickness), medium-wave emitter 15 minutes and short-wave emitter 10 minutes (of which 2 minutes at 50 % output and 8 minutes at 100 % output)
Further processing
- Dry sanding with dual-action sander and dust extraction, abrasive paper grit P400-500
- Wet sanding with abrasive paper grit P800-1000
Overcoating
Can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat
Special Notes
Elasticizing of rigid and semi-rigid plastics:
- The base material must first be mixed with 15 % elasticizer -ALZ 011 001-.
- For "wet-on-wet" processing with 2K HS hardener 2:1 and 30 % mixing filler additive -LZS 811 000 A2-
- For "wet-on-wet" processing with 2K VHS hardener 3:1 and 40 % mixing filler additive -LZS 811 000 A2-
- For processing "as sanding filler" with 2K HS hardener 3:1 and 10 % thinner
- For processing "as sanding filler" with 2K VHS hardener 4:1 and 20 % thinner
- Before applying waterborne basecoat, the minimum flash-off time increases to 45 minutes at +20 °C room temperature.
- The oven drying time for use "as sanding filler" increases to 45 minutes.
- Any defects in the substrate can be spot-filled with 2K polyester putty. After drying and interim sanding, seal the putty spots with 2K HS mixing filler.
- The best insulating effect (including on critical substrates) is achieved with a medium film build of 60-120 µm in 2 spray passes, with air drying overnight or oven or infrared drying. On critical substrates, fine preparation work is required and the parts must be filled over the entire surface.
- For isolating thermoplastic paint systems, we recommend the 2K HS Variofiller -LGF 786 004 A4-, color gray.
- For air drying, a minimum temperature of +8-15 °C is recommended when using the extra-short 2K HS hardener -LHA 009 046 A2-.
Personal protective equipment:
- Observe the safety data sheet
- Wear personal protective equipment during application
Characteristics
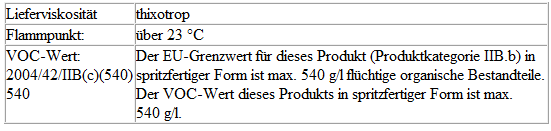
Storage
The guaranteed storage stability is 24 months (mixing filler additive 48 months) from the production date. Must be used by the date stated on the label when stored in sealed original containers at +20 °C.
2K HS Performance Filler
Designation:
- 2K HS Performance Filler -LVM 014 100 A4-, colour white
- 2K HS Performance Filler -LVM 014 173 A4-, colour dark grey
- 2K HS Performance Filler -LVM 014 190 A4-, colour anthracite
Product description
The 2K HS Performance Fillers are very high-quality 2K HS sanding fillers based on acrylic resin.
Features:
- fast drying
- very good spray mist absorption
- excellent sag resistance
- very good sandability
- high solids = high yield
Application information
Substrate
Suitable substrates:
- cleaned and sanded steel panels primed with 2K wash primer -LHV 043 000 A2- or 1K wash primer -LVM 044 007/171 A2-, electrolytically/galvanically galvanized steel panels, or soft aluminium
- lightly or unsanded, thoroughly cleaned original factory primer
- sanded factory or old paint finish (except TPA)
- surfaces pre-worked with 2K polyester products and then finely sanded
- cleaned and sanded UP-GF substrates free of release agents
Pretreatment of substrates:
- Clean thoroughly with silicone remover -LVM 020 000 A5- or long-acting silicone remover -LVM 020 100 A5-.
- Then sand.
- Use a suitable cleaner before overcoating to ensure a clean, residue-free surface.

Note
It is recommended to stir the 2K HS Performance Filler -LVM 014...- in the mixing machine.
Processing
Mixing ratio:
- 5:1 by volume with:
- 2K VHS Performance Hardener -LVM 009 038 A2-
- 2K VHS Performance Hardener, long -LVM 009 039 A2-
- (For very high technical resistance)

Note
- Mixing by weight is possible with the help of Wizard-Plus.
- Observe the national explosion protection regulations.
Elasticizing, see
Processing/pot life:
- Sprayable after 45-75 minutes at +20 °C (depending on the hardener used and the thinner addition)
Thinner:
- 2K thinner -LVE 009 001 A5-
- 2K thinner, long -LVM 009 300 A2-
- 2K thinner, plus -LHA 014 000 A5-
- 2K thinner, special -LVM 009 200 A2/A5-

Application method "Spray pass"
- Application viscosity 4 mm at +20 °C, DIN 53211
Processing viscosity, 4 mm flow cup "Compliant" and "HVLP": mixing viscosity.
Hardener addition at +20 °C material temperature of 10-15 % VHS Performance Hardener
- When adding hardener, use a measuring stick for mixing.
- Set the spray nozzle (see manufacturer's specifications): "Compliant" 1.4-1.8 mm.
- Set the spray nozzle (see manufacturer's specifications): "HVLP" 1.7-1.9 mm.
- Set the spray pressure (see manufacturer's specifications): "Compliant" 1.5-2.0 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- To achieve the recommended dry film thickness of 60-250 µm, 1-3 spray passes (with flash-off time between passes) are required.
Drying
The material can be sanded after 2-3 hours (film thickness of 60-150 µm and after air drying at +20 °C room temperature).
If film thicknesses of 150-250 µm have been applied, allow to dry overnight before sanding.
The final flash-off time with forced drying is at least 5-15 minutes.
Forced drying at +60 °C object temperature, 60-150 µm: 15-20 minutes; 150-250 µm: 20-25 minutes
The final flash-off time with infrared drying is at least 5-10 minutes.
Infrared drying (depending on film thickness), short-wave emitter 10 minutes (of which 2 minutes at 50 % output and 8 minutes at 100 % output)
Further processing
- Dry sanding with dual-action sander and dust extraction, sandpaper grit P500-600
- Wet sanding with abrasive paper grit P800-1000
Overcoating
Can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat
Special Notes
Elasticizing of rigid and semi-rigid plastics:
- The base material must first be mixed with 15 % elasticizer -ALZ 011 001-. 4:1 mixing ratio with VHS Performance Hardeners and 10 % thinner.
- Any defects in the substrate can be spot-filled with 2K polyester putty. After drying and interim sanding, seal the putty spots with 2K VHS Performance Filler.
- The best isolation effect (including on critical substrates) is achieved with a medium film build of 80-120 μm in 2 spray passes, with air drying overnight or oven or infrared drying. On critical substrates, fine preparation is required and the parts must be filled over the entire surface.
- For isolating thermoplastic paint systems, we recommend the 2K HS Variofiller -LGF 786 004 A4-, color gray.
- For air drying, a minimum temperature of +15 °C is recommended.
Personal protective equipment:
- Observe the safety data sheet
- Wear personal protective equipment during application
Characteristics
Storage
The guaranteed storage stability is:
- 2K HS Performance Filler -LVM 014...- 24 months from the production date.
- 2K VHS Performance Hardener -LVM 009 038 A2- 12 months from the production date.
- 2K VHS Performance Hardener, long -LVM 009 039 A2- 36 months from the production date.
Must be used by the date stated on the label when stored in sealed original containers at +20 °C.

2K Plastic Adhesion Primer Filler
Designation:
- 2K Plastic Adhesion Primer Filler -LKF 696 009 A2-, colour white
- 2K Plastic Adhesion Primer Filler -LKF 696 040 A2-, colour black
Product description
The 2K Plastic Adhesion Primer Filler is a high-quality 2K primer filler for plastic parts.
Features:
- Adhesion on all common passenger car plastics
- Can be used wet-on-wet
- efficient painting system
- easy to use
- very long pot life
Application information
Substrate
Suitable substrates:
- all common exterior plastic parts of vehicles
- PP, PP/EPDM, ABS, SAN, PC, PA, PUR-RIM, R-TPU, TPO, PBTP, PVC
- PUR, PUR-Weichschaum
- UP-GF
Pretreatment of substrates:
The substrate must be free of release agents.
Before cleaning, temper plastic parts for 60 minutes at +60 °C so that the release agents "sweat out".
- Clean with plastic cleaner, antistatic -LVM 001 001 A2- or with the milder silicone remover, long -LVM 020 100 A5-.

Note
- The effort required for cleaning depends on the type and amount of release agent used. To support cleaning, we recommend using a sanding pad.
- Allow the thinner to flash off thoroughly (e.g. by air drying overnight at room temperature or 30-40 minutes at +60 °C).

- Before applying the adhesion primer, clean again lightly with antistatic plastic cleaner -LVM 001 001 A2- or long-acting silicone remover -LVM 020 100 A5- (antistatic effect).

Processing
Thinner:
- Do not add any thinner!
Mixing ratio:
- 1:1 by volume with 2K adhesion primer hardener -LHA 005 000 A2-.
Processing/pot life:
- Ready-to-spray after 7-9 hours at +20 °C

Note
Do not add any thinner! The material is ready to spray after the hardener has been added.
Application method "Spray pass"

- Application viscosity 4 mm at +20 °C, DIN 53211
Application viscosity, 4 mm flow cup, "Compliant" and "HVLP" spray guns:
DIN 4 mm: 16-18 seconds
ISO 4 mm: 37-45 seconds

- Set spray nozzle (see manufacturer's specifications): "Compliant" 1.3–1.4 mm.
- Set the spray gun nozzle (see manufacturer's instructions): "HVLP" 1.4-1.5 mm.
- Set spray pressure (see manufacturer's specifications): "Compliant" 2.0–2.5 bar.
- Set atomizing air pressure (see manufacturer's specifications): "HVLP" 0.7 bar.
- Apply one coat (apply a thin first pass and follow with a normal full pass).
- The recommended dry film thickness is 25-30 µm.
Drying
Air drying at +20 °C room temperature, can be overcoated after 15-20 minutes
Overcoating

After a flash-off time of 15-20 minutes (up to max. 24 hours) at +20 °C, can be overcoated wet-on-wet with a suitable topcoat.

Note
- If necessary, the 2K plastic adhesion primer can be lightly sanded with wet sanding paper, grit P 800-1000, after 30 minutes drying (+60 °C object temperature) or after 2 hours drying (+20 °C room temperature).
- Any substrate defects can be spot-filled with 2K fine filler -LSP 784 002 A2- after the 2K plastic adhesion primer has dried.
- Filler areas must be sealed with 2K plastic adhesion primer before applying the topcoat.
Then can be overcoated with:
- Waterborne basecoat and 2K HS clearcoat
- 2K HS topcoat

WARNING!
Painted plastic parts must not be cleaned with a high-pressure washer within 6 weeks. After that, maintain a minimum nozzle distance of 30 cm from the object.
Personal protective equipment:
- Observe the safety data sheet
- Wear personal protective equipment during application
Characteristics

Storage
Guaranteed storage stability is 24 months from production date. Use by the date stated on the label at the latest when stored in sealed original containers at +20 °C.

Storage conditions
The prescribed storage temperature for the 2K plastic adhesion primer is +20 °C.
The prescribed storage temperature for the 2K adhesion primer hardener is +20 °C (must not fall below +5 °C). After exposure to frost, the hardener must be warmed back to +20 °C. It is then fully usable again.
2K HS wet-on-wet surfacer
Designation:
- 2K HS wet-on-wet surfacer -LVM 013 008 A4-, light grey
- 2K HS wet-on-wet surfacer -LVM 013 905 A4-, black
Product description
The light grey 2K HS wet-on-wet surfacer is a high-quality, VOC-compliant 2K HS wet-on-wet surfacer based on acrylic resin.
Features:
- very good application properties
- long pot life
- good flow
- fast mixing and recoating
- for efficient wet-on-wet application, especially with waterborne basecoats
- very good sag resistance
Application information
Substrate
Suitable substrates:
- cleaned and sanded steel panels primed with 2K wash primer -LHV 043 000 A2- or 1K wash primer -LVM 044 007/171 A2-, electrolytically/galvanically galvanized steel panels, or soft aluminium
- lightly or unsanded, thoroughly cleaned original factory primer
- Well-sanded original or old paint finish
- surfaces pre-worked with 2K polyester products and then finely sanded
- cleaned and sanded UP-GF substrates free of release agents
Pretreatment of substrates:
- Carefully with silicone remover -LVM 020 000 A5- or silicone remover,