Cylinder Block
GENERAL INFORMATION

Checking the flatness of the cylinder head mating surface.
1. STRAIGHT EDGE.
2. FEELER GAUGE
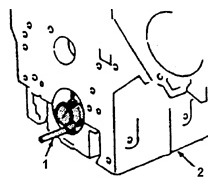
Measuring the main bearing bore diameter
1. INSIDE MICROMETER.
2. CYLINDER BLOCK
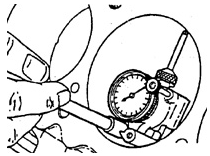
Measuring cylinder taper and out-of-round
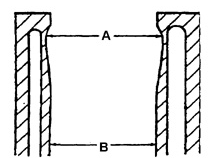
Worn cylinder profile
Disassembly
PROCEDURE.
1. Remove the coolant jacket plugs..
1a. Select a suitable self-tapping bolt..
1b. Drill a hole in the plug..
1c. Screw in the self-tapping bolt..
1d. Remove the plug..
2. Remove the threaded oil gallery plugs..
3. Remove the camshaft bearings..
Warning.
Cleaning solutions containing caustic soda damage the material of the
bearings. Therefore, bearings exposed to such
solution must be replaced. Do not clean bearings or aluminum parts
with caustic soda solutions..
Clean.
PROCEDURE.
1. Remove any sealant residue from mating surfaces..
2. Oil galleries..
3. All blind holes..
4. Clean cylinder bores and other machined surfaces with engine
oil..
Inspection
PROCEDURE.
1. Deviation from flatness of the cylinder block top face. To check,
use a straight edge and a set of feeler gauges, Fig. Checking
the cylinder head mating surface flatness. Minor
irregularities can be carefully removed..
2. Check the oil pan and camshaft cover mating surfaces for dents. Minor defects can be removed with a thin flat
file..
3. Transmission housing mating surface of the cylinder block..
Warning.
A deformed mating surface may cause damage to the drive plate with
ring gear (fitted with automatic transmission)..
4. Temporarily install the crankshaft. Measure the runout of the shaft flange..
5. Threaded holes. If necessary, clean the threads..
Repair damaged holes using thread inserts..
Warning.
Further inspection and restoration of parts must be performed with the
caps installed and tightened to the specified torque.
main bearing caps..
6. Make sure the main bearing caps are installed correctly. The arrows on the
caps must point toward the front of the engine..
7. Bearing bores condition. Measure the bore diameters with an inside micrometer,
check the alignment of the crankshaft and camshaft bearing bores. If out of specification, replace the cylinder block. If there are defects on the outer surfaces of the bearing inserts, carefully remove minor
irregularities from the bearing seats..
8. Check the cylinder bores for wear, out-of-round and taper with an
inside micrometer, Fig. Measuring cylinder taper and out-of-round.
9. If the cylinders are worn, they can be bored and honed to the next
repair size. In this case, install oversize pistons and rings in the engine.
of the corresponding oversize..
Warning.
When machining the cylinders, leave the necessary allowance for the honing
operation to the final size corresponding to the piston diameter..
10. If the cylinder bores have film deposits and are still serviceable,
remove these deposits with a hone and replace the piston rings.
piston rings..
11. Before honing the cylinders, make sure the honing stones are clean and in proper shape. Move the hone slowly along the cylinder axis to obtain a correct surface finish (the crosshatch lines should be at
the proper angle)..
at a 45-degree angle to the cylinder axis). After honing, be sure to thoroughly
wash the cylinder bores with soapy water, dry, and lubricate with engine oil.
oil. Perform control measurements of the cylinders.
Assembly.
PROCEDURE.
1. Install the water jacket plugs in place. Use sealant of the specified type.
1050026..
2. Install the threaded oil gallery plugs in place. Bearings.
camshaft.
Test yourself
A quick Daewoo Nexia quiz: every answer comes with an explanation and a link to the manual page.