Overview of riveting attachments
In this manual: Overview of riveting attachments
~2min read
The listed pairs only serve as a guideline. Refer to the provided operating instructions for a description of the work procedure and areas of application.
Important
To extend the service life of the snap dies, use a commercially available cutting fluid.
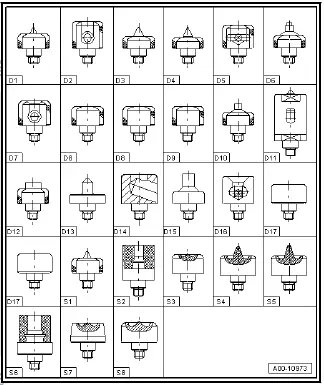
- D 1 + D 2 - Pressing out
 3.2 mm punch rivet
- D 2 + D 3 - Pressing out
 3.2 mm punch rivet
- D 2 + D 5 - Pressing out
 5 mm punch rivet
- D 3 + D 5 - Pressing out
 5 mm punch rivet
- D 4 + D 5 - Pressing out
 5 mm punch rivet
- D 5 + D 12 - Hole punching
 8 mm hole for welded joint
- D 6 + D 7 - Hole stamp for
 4.8 mm pop rivet
- D 8 + D 8 - Bending panel back into its original shape
- D 8 + D 9 - Hole stamp for
 4 mm solid rivet
- D 8 + D 9 - Hole punching and stamping for
 4 mm solid rivets
- D 13 + D 14 - Pressing out
 5.3 × 7.5 mm punch rivet
- D 17 + D 17 - Bending panel back into its original shape
- D 15 + D 16 - Hole stamp for
 6.0 mm solid rivet
- D 17 + D 17 - Hole stamp for
 6.0 mm solid rivet
- S 1 + D 2 - Pressing out
 3.2 mm punch rivet
- S 2 + S 3 - Setting
 3.2 mm punch rivet
- S 4 + D 5 - Pressing out
 5.3 × 5.5 mm punch rivet
- S 5 + D 5 - Pressing out
 5.3 × 6.5 mm punch rivet
- S 6 + S 7 - Setting
 5.3 × 5.5 mm punch rivet
- S 6 + S 8 - Setting
 5.3 × 6.5 mm punch rivet
Flow-drill screws
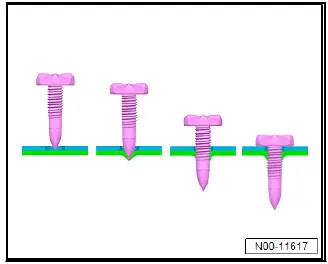
When using flow-drill screws, the lower component is heated through the frictional heat of the rotating screw, and the selftapping screw cuts into the soft aluminium.
Repairing joints with flow-drill screws (FDS)
- ⇒ Rep. gr. 52 ; Making a flow-drill screw connection, predrilled hole in upper part
- ⇒ Rep. gr. 52 ; Making a flow-drill screw connection, no pre-drilled hole in upper part
- ⇒ Rep. gr. 52 ; Making a flow-drill screw connection, exchanging upper and lower parts
Was this page helpful?